Selecting aluminum windows requires understanding material grades, extrusion processes, and coating standards. This guide explains how procurement managers can evaluate frame quality, verify compliance, and avoid common specification errors during window procurement.
- Material grade determines structural strength and corrosion resistance, so verify the alloy specification before pricing.
- Surface treatment standards protect the frame against weathering and UV exposure.
- Procurement documents must align with project standards to prevent rework.
- Cross-check supplier certifications against your project requirements.
- Physical inspection of samples reduces the risk of receiving non-conforming stock.
Why Material Grade Matters More Than Finish
Aluminum windows are often judged by their appearance. That is a mistake. The finish is the outermost layer. The alloy grade and extrusion quality sit underneath. A bright silver or dark grey coating looks the same on a weak alloy and a strong one.
For procurement, the grade dictates performance. A structural frame must resist sagging under its own weight and the pressure of wind loads. A window that sags will lose its thermal break function and its weather seal.
Most architectural aluminum uses 6061 or 7000 series alloys. The 6061 series is the workhorse for general construction. It balances strength, workability, and cost. The 7000 series offers higher yield strength for larger spans or heavier glazing.
When reviewing a supplier quotation, do not accept “aluminum” as the material description. Request the specific alloy designation. Ask for the heat treatment condition as well, often expressed as T6. Without this, the metal may have been extruded but not properly strengthened.
Consider a standard office window opening. The frame carries the glass, the sash, and the hardware. It also stands against the wind pressure pushing against the glazing. If the alloy is too soft, the vertical mullion will bow over time. This bowing pulls the sash out of alignment. The gasket loses contact with the frame. Water starts to enter during heavy rain. The fix is not just to paint over the gap. It requires replacing the structural member.
The difference between 6061 and 7000 series is not just in the numbers. It is in the mechanical behavior. 6061-T6 is a solid choice for most residential and commercial units. It extrudes cleanly and machines well. If you are building a curtain wall with large, fixed panes or a high-rise structure with significant wind deflection, the 7000 series provides the necessary stiffness. It resists bending better under load.
Heat treatment is the hidden variable. Extrusion changes the crystal structure of the metal. Without proper tempering, the aluminum is soft. T6 tempering involves aging the metal at a specific temperature to increase hardness. When you ask a supplier for the alloy, always ask for the temper. A 6061 profile without a stated temper is a liability. It may be 6061-O (annealed) or 6061-T652. The mechanical properties differ significantly.
In a bid evaluation, look for the mill certificate. This document from the metal supplier confirms the chemical composition and the heat treatment batch. Without it, you are relying on the fabricator’s word. In a competitive bidding environment, vague answers are a red flag. If a supplier cannot provide the mill certificate for the specific lot of aluminum, assume the material may not meet the design requirements.
How to Evaluate Extrusion Quality
Extrusion is the process of forcing molten metal through a die. The quality of the die and the cooling rate determine the internal grain structure.
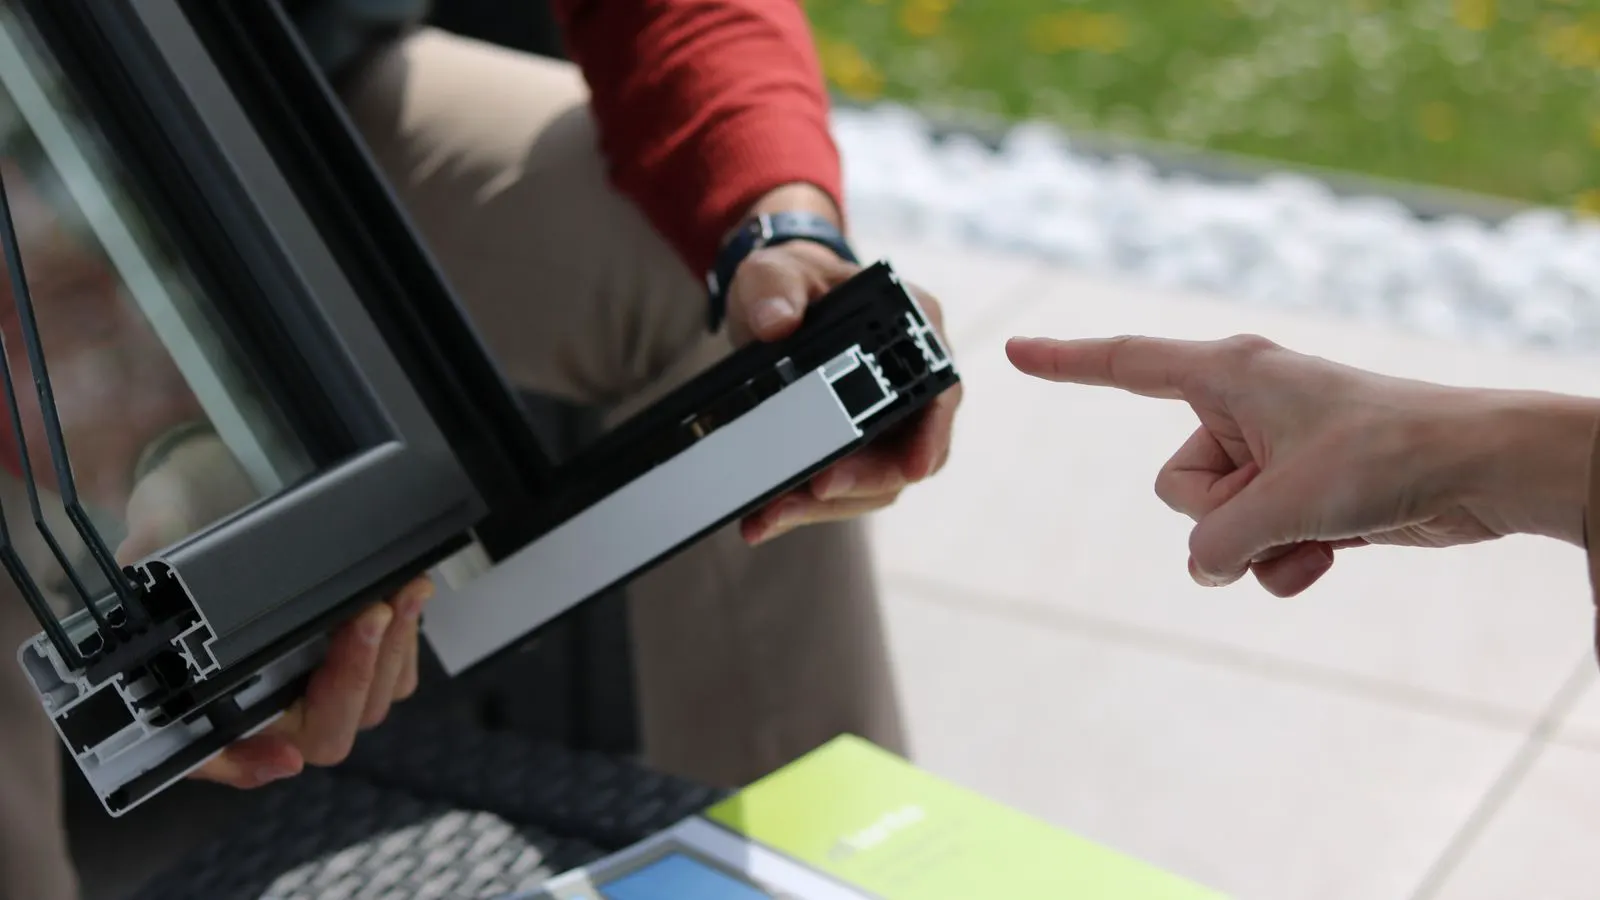
Look for the following during sample inspection:
- Surface finish. The profile should be uniform. Check for pitting, streaks, or porosity.
- Dimensional tolerance. Measure the wall thickness. Thin walls compromise the frame’s rigidity.
- Corner joints. Extruded profiles often have mitered corners. Check for gaps. A gap indicates poor machining.
- Anodizing or painting. Check the adhesion. Scratch the coating lightly with a fingernail. It should not flake.
A common specification error is specifying a minimum wall thickness without specifying the profile design. A thin wall on a complex profile may fail. A thick wall on a simple profile may be over-engineered and expensive.
The profile design should match the opening size. Large openings need deeper profiles to resist deflection. Small openings can use standard depths.
Extrusion quality is visible in the details. When you pick up a sample, run your hand along the length of the profile. You should feel a smooth, consistent surface. Any roughness or ridges indicate a worn die or a problem in the extrusion line. These imperfections can trap moisture and accelerate corrosion at the base of the profile.
Wall thickness is not just about weight. It is about bending stiffness. A profile with a 1.5mm wall may look fine in a small window. In a large fixed pane, that same wall thickness will deflect. The glass will show stress fractures or the frame will vibrate in high winds. For larger spans, you need a deeper extrusion or a thicker wall. The engineer calculates the required section modulus. You need to ensure the supplier’s profile matches that calculation.
Corner joints reveal the machining precision. Most modern windows use mitered corners cut at 45 degrees. The gap between these cuts must be tight. A visible gap allows air and water to bypass the seal. It also makes the unit look cheap. If the corner has a gap, the machining tool is not sharp or the alignment is off. This is a quality control failure.
Coating adhesion is a simple check. Use a fingernail or a soft cloth to rub the surface. If paint or anodizing lifts, the surface preparation was poor. Aluminum is naturally corrosive. The coating must bond to the metal. If it fails, the metal underneath will corrode and blister the coating. This is a common failure mode for low-quality coated profiles.
Surface Treatments and Durability Standards
Aluminum reacts with moisture and UV light. Surface treatment is the defense.
Anodizing is an electrochemical process. It creates a hard oxide layer on the metal. It is highly durable and requires little maintenance. It is common for premium architectural applications.
Thermoplastically coated profiles are also common. The coating is applied to a pre-primed profile. It offers a wider color range than anodizing. The quality of the primer is critical. Poor priming leads to blistering over time.
When specifying, define the coating standard. Look for documentation that meets recognized international requirements for adhesion, thickness, and colorfastness.
For coastal or humid environments, consider the environment. Salt spray resistance becomes a factor. Anodized profiles generally handle this well. Coated profiles need a high-quality primer system.
Anodizing creates a layer that is part of the metal. It is extremely hard and resistant to abrasion. The thickness of the anodized layer is measured in microns. A standard architectural anodize is typically 10 to 25 microns. It is not as thick as a paint layer, but it is chemically bonded. This makes it very durable in harsh weather. However, anodizing limits the color palette. You can get silver, bronze, and some darker shades, but bright reds or blues are difficult to achieve with a consistent finish.
Coated profiles use a liquid or powder coating system. The profile is first treated with a primer to improve adhesion and corrosion resistance. Then the topcoat is applied. This system allows for virtually any color. It is popular for projects where the aluminum must match a specific architectural design. The downside is the complexity of the system. If the primer fails, the topcoat fails. Blistering is a common sign of primer failure. It often appears after a few years of exposure.
When specifying a coating, you must specify the standard. Do not just say “painted aluminum.” Ask for the coating thickness in microns. Ask for the adhesion standard. Ask for the salt spray resistance test results. A coating that has passed a 500-hour salt spray test is different from one that has only passed a 100-hour test. For a coastal building, you need the higher standard.
Consider the maintenance implications. An anodized profile can be cleaned with water and a soft brush. It will not need repainting. A coated profile may need repainting after 10 to 20 years, depending on the exposure. The coating is a consumable. The metal is the structure. You are buying a finish that has a lifespan.
Understanding Standards and Compliance
Window procurement involves a web of standards. These standards cover the material, the testing, and the performance.
You need to distinguish between material standards and performance standards. Material standards define the chemical composition and mechanical properties of the aluminum. Performance standards define how the window performs in the field.
For a global project, you must identify which regional standard applies. The building code dictates the minimum performance. The material standard ensures the material is fit for that performance.
If you are in a region with specific building codes, verify that the supplier’s test reports align with those codes. A window that passes a generic test may fail a regional one.
Do not assume that a supplier’s internal quality control is sufficient. Request third-party test reports for critical components. This is especially true for the thermal break and the gaskets.
Standards are the language of compliance. They tell you how the product was made and how it was tested. Material standards, such as those for aluminum alloys, specify the maximum levels of impurities like iron or silicon. They ensure the metal behaves predictably under load. If the alloy is out of spec, the window may fail structurally.
Performance standards are about the finished unit. They test the window as a whole. They measure air leakage, water infiltration, and impact resistance. They also test thermal performance, measuring the U-value of the window. These tests are performed in a laboratory using standardized methods. The results are reported in a test certificate.
Regional variations are significant. A window that meets the energy efficiency requirements of one country may not meet those of a neighboring country. The climate zones differ. The building codes differ. You must identify the specific code that applies to your site. The local authority having jurisdiction (AHJ) will require a specific set of test reports.
Third-party testing is the gold standard. A supplier’s internal QC checks are good for detecting obvious defects. They are not enough for verifying compliance. An independent laboratory, accredited to international standards, tests the sample. They issue a report that lists the test methods and the results. This report is valid for the specific model and configuration tested. Do not assume that a report for one model applies to a similar model. The geometry, the glazing, and the hardware all affect performance.
When reviewing a supplier’s documentation, look for the scope of the test. Does it cover the specific frame size you are buying? Does it include the specific glazing unit? If the test was done on a different configuration, you need a new test or a performance prediction report from a qualified engineer.
Common Procurement Mistakes to Avoid
Procurement managers often focus on unit price. This leads to two main problems.
First, you buy the cheapest grade. The savings on the material are wiped out by higher maintenance costs or structural failures.
Second, you specify vague requirements. “High quality aluminum” is not a specification. It is a hope.
Here are the typical errors:
- Missing alloy specification. The quote says “aluminum.” You need “6061-T6.”
- No coating standard. You get whatever the supplier has in stock.
- Ignoring the thermal break. The frame is strong, but the insulation is poor.
- No sample approval. You approve the drawings, but not the physical sample.
- Vague delivery terms. You do not specify the packaging or the handling instructions.
To fix these, create a standard technical specification sheet. Include the alloy, the wall thickness, the coating, and the required test reports.
Use this sheet for every project. It reduces negotiation and ensures consistency.
The cost of a window is not just the metal. It is the installation, the maintenance, and the performance over the building’s life. If you save 5 percent on the alloy grade, but the window leaks or sags, the repair cost will be far higher than the savings. A sagging frame is difficult to fix. It often requires cutting out the section and replacing it with a new piece of aluminum. This involves demolition, waste, and labor.
Vague specifications lead to supplier discretion. If you do not specify the coating thickness, the supplier will use the thinnest coating they have in stock. It may look fine in the showroom, but it will fail in the field. If you do not specify the sample approval, the supplier will ship the first batch they have made. It may not match the approved sample. You end up with a mismatched finish on the building.
Sample approval is a critical step. You must approve the physical profile, not just the drawing. The drawing shows the shape. The sample shows the material quality. The sample shows the finish. The sample shows the corner joints. You need to see and touch the actual product. If the sample fails, you stop. Do not proceed.
Delivery terms matter for preservation. Aluminum is a soft metal. It can be scratched or dented during handling. If the delivery terms do not specify proper packaging, the profiles may arrive damaged. Scratches in the coating can lead to corrosion. Dents in the frame can affect the fit and the function. Specify that the materials must be packaged to prevent damage in transit.
A Practical Comparison of Material Grades
Different grades serve different purposes. The table below summarizes the typical trade-offs.
| Criterion | What to look for | Why it matters |
|---|---|---|
| Alloy Grade | 6061-T6 for standard, 7000 series for high strength | Determines structural integrity and deflection resistance |
| Wall Thickness | Consistent thickness, typically 1.5mm to 2.5mm | Thin walls sag. Thick walls are rigid but cost more |
| Surface Treatment | Anodized or coated with specified thickness | Protects against corrosion and UV degradation |
| Thermal Break | Insulated barrier between frame and sash | Reduces heat transfer and condensation risk |
| Gasket Material | EPDM or silicone | Ensures long-term weather tightness |
The alloy is the skeleton. The coating is the skin. The thermal break is the insulation. You need all three to work together.
A 6061 alloy with a poor coating will corrode. A 7000 alloy with a thin wall will still sag if the profile is too shallow. The specifications must be holistic.
The interaction between these elements is complex. A high-strength alloy allows for a thinner wall, which reduces weight and cost. But if the wall is too thin, the surface treatment may be harder to apply evenly. A thick wall is easier to coat, but it is heavier and more expensive. You must balance these factors.
The thermal break is often an afterthought in procurement. It is a critical component for energy efficiency. It is a plastic or polymer strip that separates the metal from the metal. It prevents heat transfer through the frame. Without a good thermal break, the window will have a high U-value. The building will lose heat in winter and gain heat in summer. The thermal break must be continuous. It must be properly installed. If the gap in the mitered corner is not sealed, the thermal break is broken. The window will perform poorly.
Gasket material affects long-term performance. EPDM is a common choice. It is durable and resistant to ozone. Silicone is also used, especially in high-temperature applications. The gasket must remain flexible over time. If it hardens, it loses its seal. The material must be compatible with the frame and the coating. Incompatible materials can cause chemical reactions that degrade the seal.
Final Decision Checklist
Before releasing the purchase order, run through this list.
- Alloy verified. The specification states the exact alloy and heat treatment.
- Coating specified. The finish type and thickness are defined.
- Thermal break confirmed. The insulation material is listed.
- Sample approved. You have physically inspected a sample of the proposed profile.
- Test reports received. Third-party reports for structural and weather performance are on file.
- Delivery terms clear. Packaging and handling requirements are stated.
If any item is missing, stop. Do not proceed with the order. A clear specification is cheaper than a claim for defective goods.
Aluminum windows are a long-term asset. The material choice is a permanent one. Take the time to verify the grade and the standards. Your building will benefit.
Frequently asked questions
What is the most common aluminum alloy for window frames?
The 6061 alloy in T6 heat treatment is the most widely used for architectural windows. It offers a good balance of strength and cost.
How do I know if a supplier’s aluminum meets the required strength?
Request the mill test certificates for the specific batch of material. These documents confirm the chemical composition and mechanical properties.
Is anodizing better than painting for aluminum windows?
Anodizing is generally more durable and requires less maintenance. It is preferred for high-visibility or harsh environments. Painting offers more color options.
What is the difference between a 6061 and a 7000 series alloy?
The 7000 series is stronger than the 6061 series. It is used for larger openings or heavier glazing where deflection must be minimized.
Do I need to specify the wall thickness in my procurement document?
Yes. Always specify the minimum and maximum wall thickness. This ensures the frame has the necessary rigidity for the opening size.